
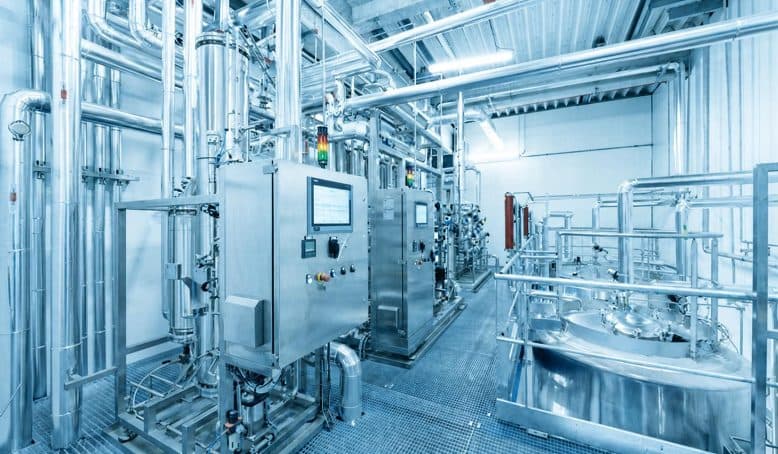
A clean utility system is judged at the outlet, not at the still. Water that leaves a generator meeting Ph. Eur. limits and arrives at the point of use contaminated by biofilm in the loop has failed, and the generator will test perfectly throughout the investigation. Almost every clean utility problem we are called to look at is a distribution problem.
Three grades, three jobs
Purified Water (PW) is the workhorse: under USP, conductivity not more than 1.3 µS/cm at 25 °C (Ph. Eur. allows 5.1 µS/cm) and TOC not more than 500 ppb. It serves non-parenteral product, equipment washing and the feed to higher grades.
Water for Injection (WFI) carries the same chemical limits with an endotoxin requirement on top, and is used for parenteral product and final rinses. It is distributed either as a hot recirculating loop, with constant circulation above 70 °C as the example EU GMP Annex 1 gives, or cold with a defined sanitization regime. Hot is simpler to defend and more expensive to run; cold is cheaper and asks more of the sanitization program.
Pure steam is steam whose condensate meets WFI quality, used for sterilization and anywhere steam contacts product. It is tested to EN 285 for non-condensable gases, dryness and superheat — because wet steam does not sterilize reliably, and neither does steam carrying air.
Where distribution systems actually fail
Dead legs. A branch that flow does not reach is where biofilm establishes. The limit is expressed as a ratio of branch length to pipe diameter (L/D) and it is a design rule, not a site preference — verified during installation, because it cannot be verified afterwards without dismantling the loop.
Drainability. A loop that cannot be fully drained cannot be reliably sanitized or reliably dried. Slope has to be drawn on the isometrics and checked on site, and it is the first thing lost when a services coordination problem is solved by lifting a pipe run.
Weld quality. Orbital welding produces a consistent internal profile with a recorded parameter set for every joint, which is why it is standard for these systems. The weld log is part of the qualification evidence, not a construction record that can be discarded at handover.
Surface finish and passivation. 316L is specified for corrosion resistance that depends on an intact chromium oxide layer. Fabrication disturbs it; passivation restores it. Skipping passivation produces a system that performs for a year and then starts contributing metal ions and rouge to the product stream.
Sanitization is designed, not scheduled
The most common costly mistake is treating sanitization as an operational decision made after handover. Whether a loop is sanitized by hot water, pure steam or chemicals determines its material selection, its slope, its instrumentation and the temperature its components must survive. Retrofitting a sanitization strategy onto a loop that was not designed for one usually means replacing it.
What to ask for
A clean utility package should hand over the isometrics with dead-leg dimensions marked, the weld log, material certificates, passivation records, the sanitization procedure with its validated parameters, and the sampling plan with each point's rationale. If a supplier cannot produce that set, the system may still be sound — but you cannot prove it, and at an inspection those are the same thing.
Industries

